Dirancang untuk bisnis Anda
Sistem robot inspeksi otomatis berkelanjutan untuk konveyor dan fasilitas industri.
Digital Transformation of Traditional Industries
Inspection Robot for Bulk Material Belt Conveyors
Belt Conveyor
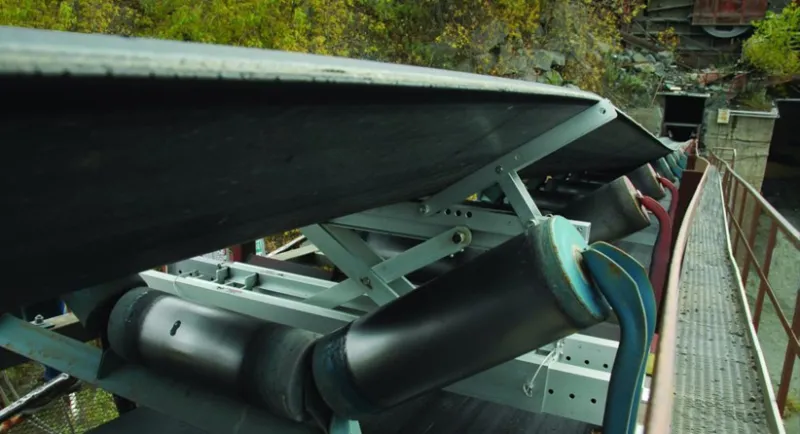
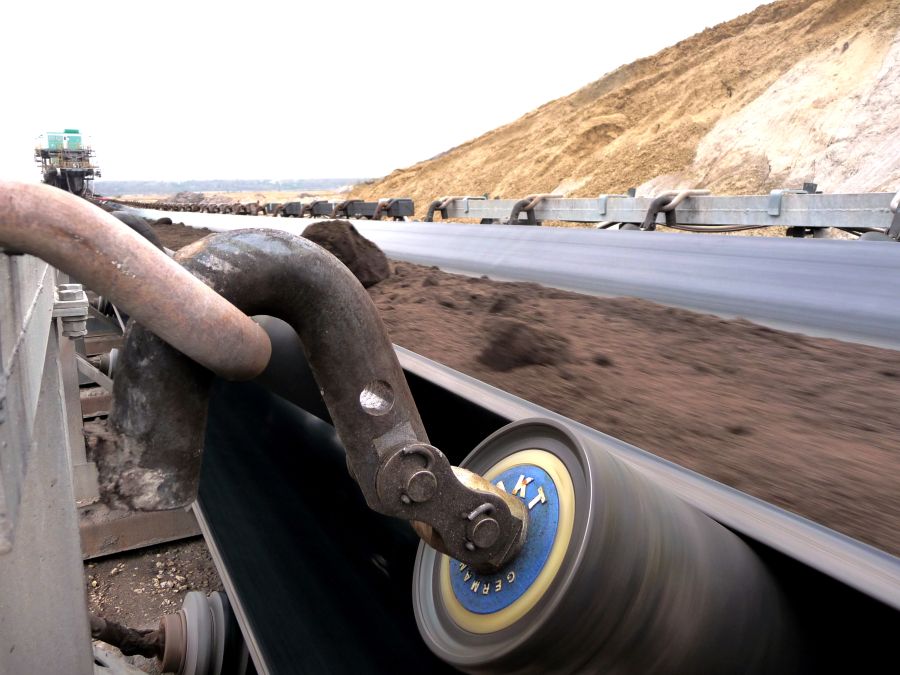
A belt conveyor is a machine that transports material continuously by friction drive. It mainly consists of a frame, conveyor belt, idlers, pulleys, tensioning device and transmission device. It forms a material conveying flow along a certain conveying line, from the initial feeding point to the final discharge point.
A belt conveyor is a complex large-scale electromechanically coupled system whose subsystems are subject to a wide variety of faults. Once a fault occurs, on-site repair is difficult and time-consuming, consumes substantial human and material resources, reduces the enterprise's economic benefits, and may even endanger personal safety.
During operation, belt conveyors encounter various fault events. To ensure safe production, it is necessary to monitor and analyze the characteristic signals corresponding to various typical states of the belt conveyor online, detect potential degradation trends in time, and eliminate faults before they occur.
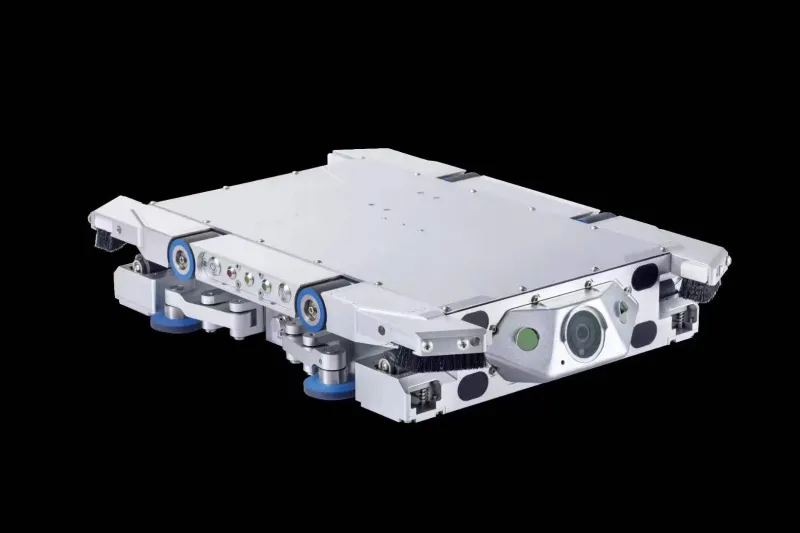
Belt Conveyor Inspection Robot
Advances in sensor technology, high-speed networking and computing power have greatly promoted the development of artificial intelligence, making it possible to combine new AI technologies with traditional industrial operation and maintenance. Using advanced sensing technology and AI machine learning to monitor key components of the belt conveyor in real time and analyze operating condition evolution enables automated and intelligent equipment O&M, reduces maintenance costs, and improves maintenance efficiency and production benefits.
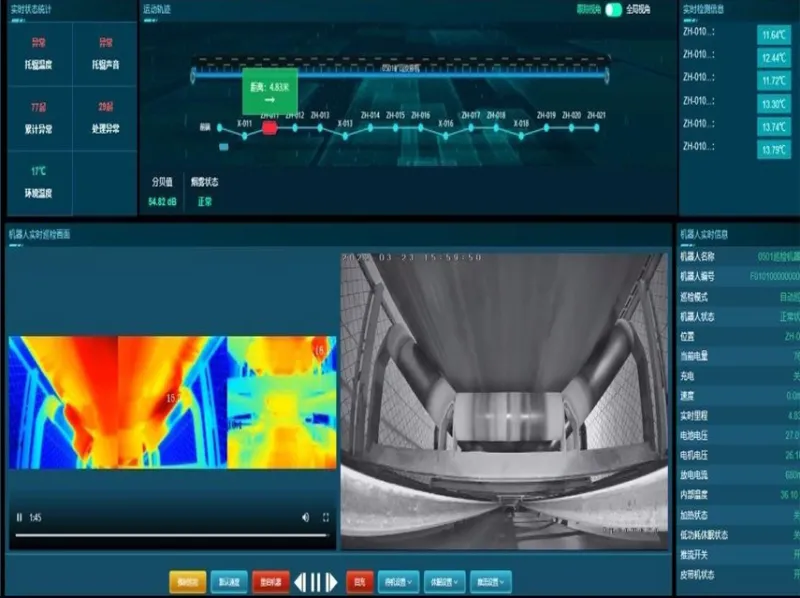
The O&M control center remotely operates the field robot in real time. Data collected by the robot is transmitted in real time through a dedicated network to the O&M control center, where operators make final judgments on the operating condition of monitored equipment based on real-time image data and analysis data.
Intelligent Monitoring
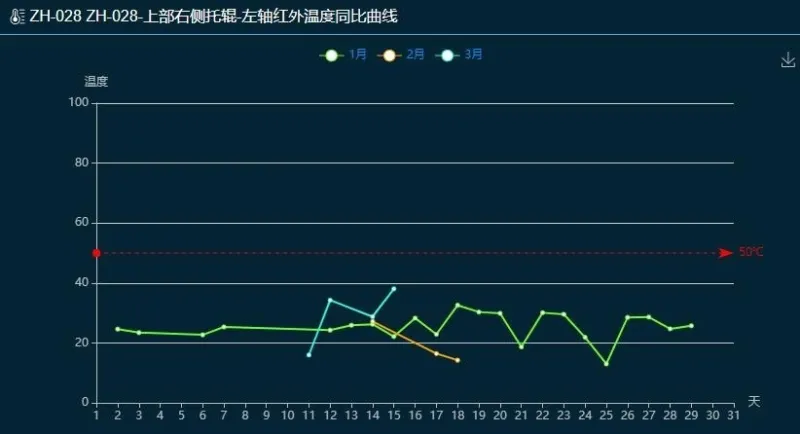
The inspection robot is equipped with three non-contact infrared thermal imaging thermometers that locate and measure the temperature of upper and lower idlers respectively. When an idler temperature rise reaches a certain threshold, the system issues an alarm. As site conditions and temperatures vary considerably, the inspection strategy uses relative temperature as the judgment basis, effectively reducing false alarms caused by environmental factors and equipment accuracy.
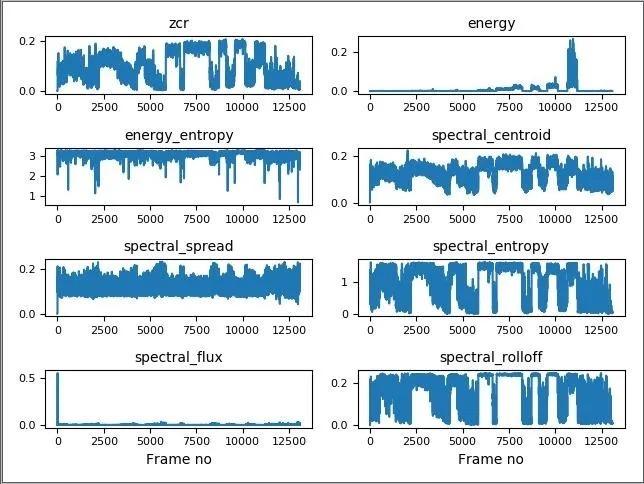
The inspection robot carries a highly sensitive microphone that collects abnormal noises from the corridor, equipment, conveyor steel frame and idlers in real time — such as loose bolts, cracked welds and frame sway. By comparative analysis against original sound samples, extracting sample features and learning classification models, it raises alarms and records anomalies.
Fault Localization and Early Warning
Advances in sensor technology, high-speed networking and computing power have greatly promoted the development of artificial intelligence, making it possible to combine new AI technologies with traditional industrial operation and maintenance. Using advanced sensing technology and AI machine learning to monitor key components of the belt conveyor in real time and analyze operating condition evolution enables automated and intelligent equipment O&M, reduces maintenance costs, and improves maintenance efficiency and production benefits.
The O&M control center remotely operates the field robot in real time. Data collected by the robot is transmitted in real time through a dedicated network to the O&M control center, where operators make final judgments on the operating condition of monitored equipment based on real-time image data and analysis data.